 WonksAnonymous
Small Batches and Frequent Changeovers: The Hidden Cost of Packaging
A model linking batch size, changeover time and run time to good packs and cost per good pack, with a worked shift example and a simple changeover log.
When a plant moves from a few long runs to many short ones, the cost rarely shows up on any single report. Wages are paid, the machine is on, and packs still come out. What goes missing is good output, and with it money, every time the line changes product. The practical question is whether to cut the number of changeovers, shorten them, or live with them.
Each changeover removes minutes of run time and a quantity of setup material, and both land on the same fixed shift cost. In the example below, doubling the changeovers on a shift raises the cost of each good pack by several percent. Fixing it doesn’t always mean larger batches.
What a changeover is
Measure a changeover from the last good pack of product A to the first good pack of product B at target speed. If you stop the clock when the machine restarts, you miss the slow minutes that follow.
A changeover has five parts:
- Stopping and clearing: ending the run, emptying product, cleaning the filling and sealing areas.
- Swapping parts and materials: format parts, film or pouches, labels, date coding.
- Adjustments: sealing temperature, weight settings, registration, guides.
- Trial packs and rejects: packs made to check seals, weights and print, most of which are scrapped.
- Ramp back to speed: running below target while settings settle.
The last three are the hidden part. Stopped time is easy to see on a clock. Setup material and the slow first minutes often get absorbed into the next batch’s reject and speed figures, so nobody ties them to the changeover that caused them.
The model
The model works per shift. Rate here means the effective running rate in good packs per minute while the line is running, already net of micro-stops, speed loss and rejects, as built up in Why Faster Machines Do Not Always Increase Line Output. Changeover losses are counted separately, so nothing is counted twice.
changeovers per shift  ~ packs demanded per shift / batch size
                         (or the number of product changes actually scheduled)

changeover time        = changeovers x minutes per changeover
run time               = planned time - changeover time - other downtime
good packs             = run time x effective running rate
setup waste            = changeovers x packs (or film meters) lost per changeover
share of shift lost    = changeover time / planned time
Cost per good pack uses the definition in Cost per Good Pack: cash operating cost for the period divided by good packs in the same period. The setup waste is made during the changeover minutes, so it doesn’t reduce the good-pack count a second time. Its cost is the material it consumed, so it enters through material spend. If your material spend comes from purchases or issues to the line, it already includes the waste, and you must not add a separate scrap line on top.
Worked example: one shift, three batch patterns
Worked example. Replace each input with a quote or a measured figure from the plant before using the result.
Assumptions for one 8-hour shift (480 minutes):
- Effective running rate: 35 good packs per minute (the 35.64 from the throughput article, rounded down).
- Changeover: 25 minutes each, including trial packs and ramp back to target speed.
- Setup waste: 60 packs per changeover.
- Other downtime (breaks, planned cleaning): 30 minutes, the same in every pattern.
- Shift labor and overhead: $1,200, fixed regardless of the pattern.
- Material: $0.08 per pack, applied to good packs and to setup waste alike.
Scroll horizontally to see all columns.
| Changeovers | Changeover minutes | Run minutes | Good packs | Setup waste (packs) | Share of shift lost |
|---|---|---|---|---|---|
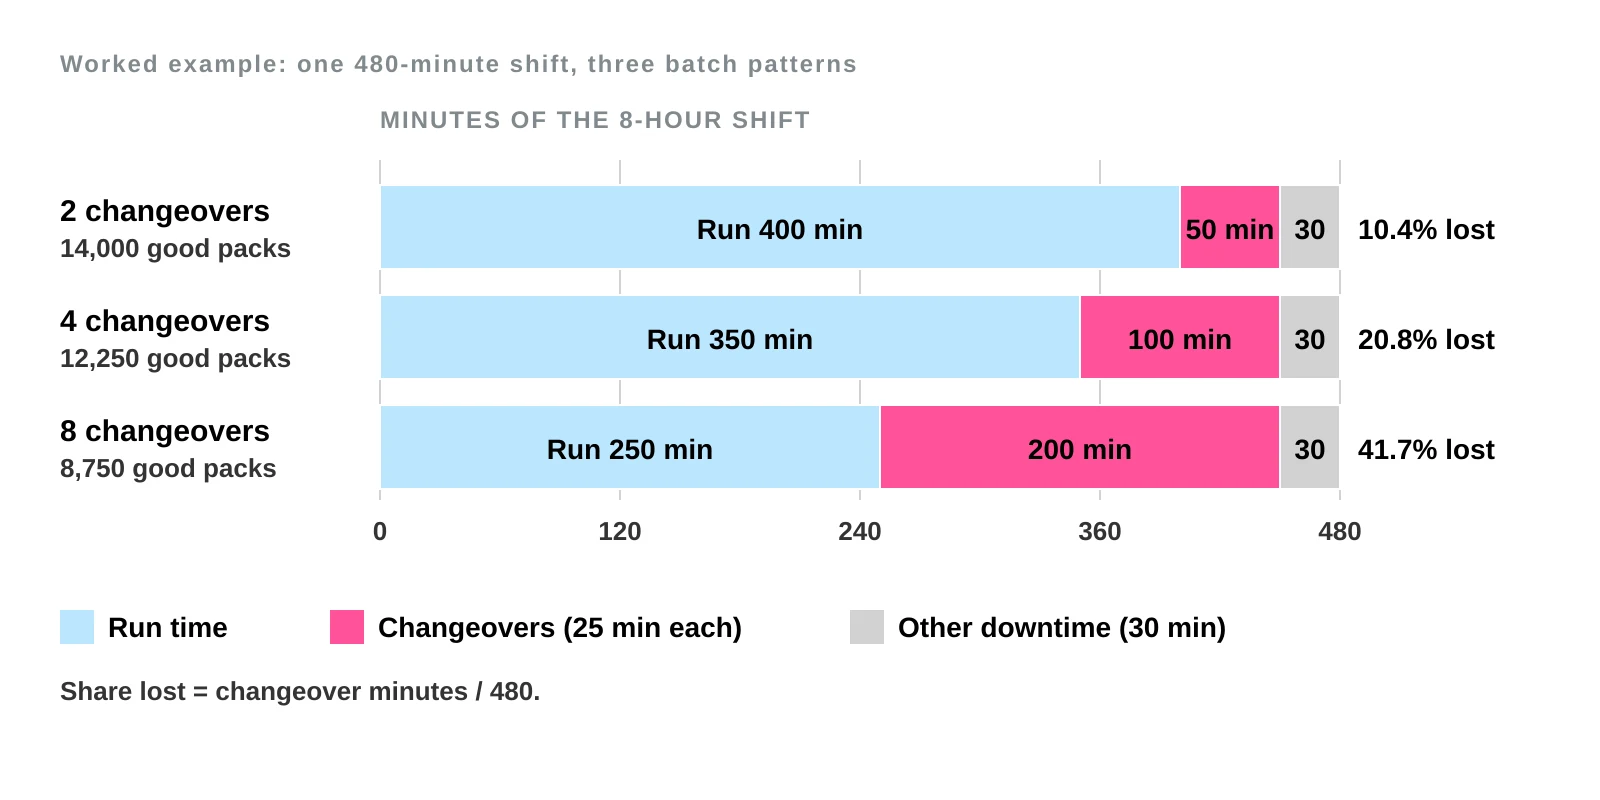
| 2 | 50 | 400 | 14,000 | 120 | 10.4% |
| 4 | 100 | 350 | 12,250 | 240 | 20.8% |
| 8 | 200 | 250 | 8,750 | 480 | 41.7% |
For the 4-changeover row: 4 x 25 = 100 minutes; 480 - 100 - 30 = 350 run minutes; 350 x 35 = 12,250 good packs; 4 x 60 = 240 packs of waste; 100 / 480 = 20.8%. The other rows follow the same steps: 2 x 25 = 50, 480 - 50 - 30 = 400, 400 x 35 = 14,000; 8 x 25 = 200, 480 - 200 - 30 = 250, 250 x 35 = 8,750.
Now the cost. Material covers good packs plus setup waste, and the $1,200 of labor and overhead is added on top.
Scroll horizontally to see all columns.
| Changeovers | Material cost | Shift cost | Cost per good pack | Cost per 1,000 good packs |
|---|---|---|---|---|
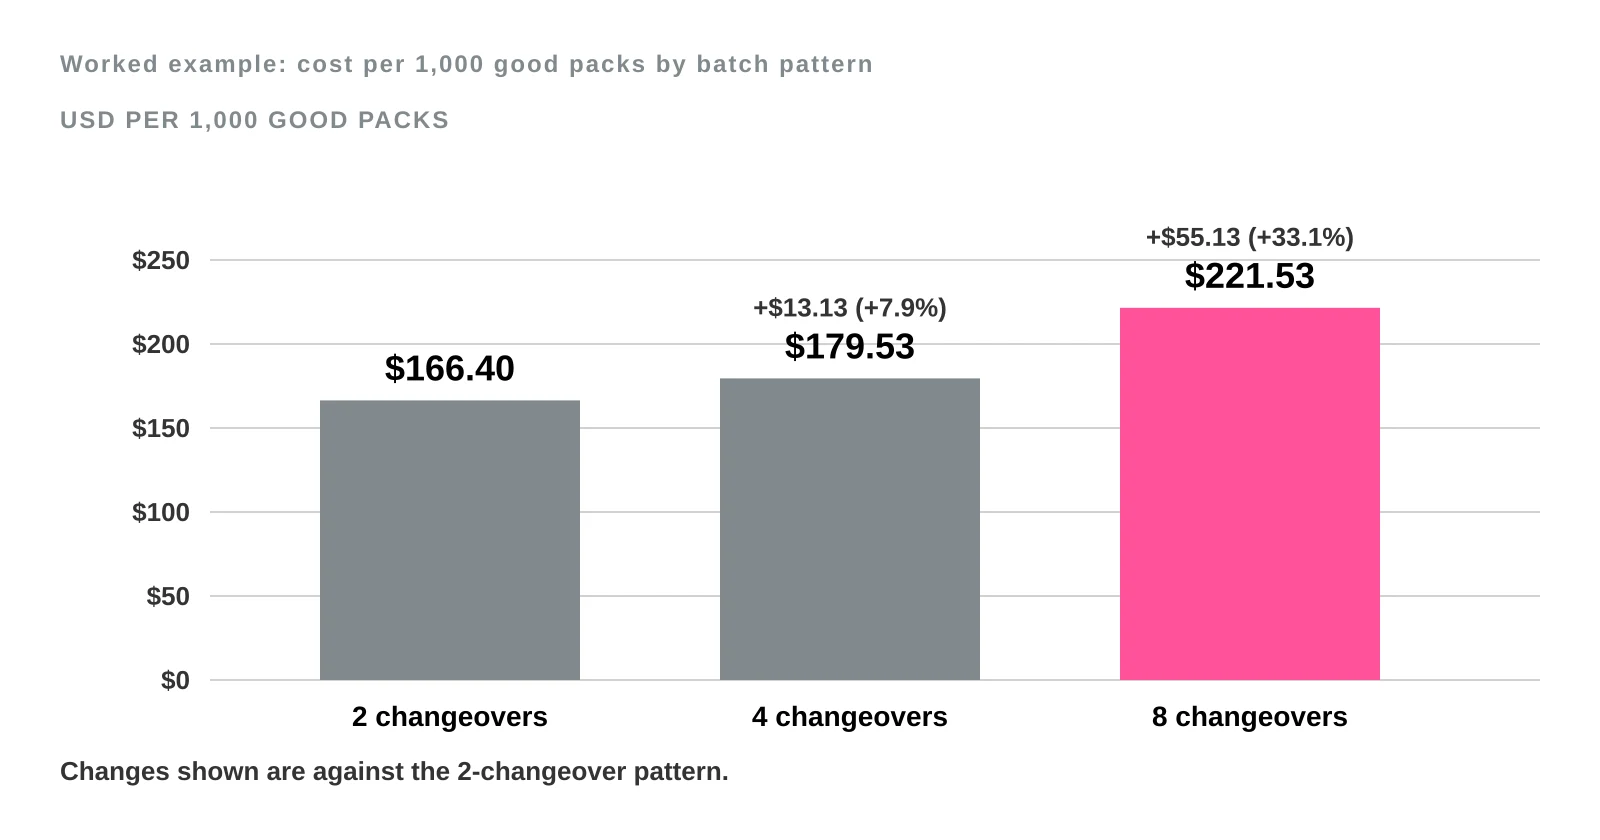
| 2 | (14,000 + 120) x $0.08 = $1,129.60 | $2,329.60 | $0.1664 | $166.40 |
| 4 | (12,250 + 240) x $0.08 = $999.20 | $2,199.20 | $0.1795 | $179.53 |
| 8 | (8,750 + 480) x $0.08 = $738.40 | $1,938.40 | $0.2215 | $221.53 |
The last column divides by thousands of good packs: $2,329.60 / 14.00 = $166.40; $2,199.20 / 12.25 = $179.53; $1,938.40 / 8.75 = $221.53.
Going from 2 to 4 changeovers raises the cost per 1,000 good packs by $13.13, or 7.9%. Going from 2 to 8 raises it by $55.13, or 33.1%. Total spending falls as the line makes less, yet each good pack costs more, because the $1,200 shift cost is spread over fewer of them. Setup waste is a small part of that rise. Most of it comes from lost run time.
Two levers
You can reduce the loss in two ways. One is fewer changeovers: larger batches and smarter sequencing, such as light colors before dark, small formats before large, and products grouped by film width or pouch size so adjacent runs need fewer part swaps. The other is faster changeovers, which means shortening the 25 minutes itself. Format and material changes, such as moving between rollstock and premade pouches, bring their own changeover work; see Rollstock Versus Premade Pouches.
To speed up changeovers, start by sorting the work into two groups. Some tasks can be done while the line is still running, such as staging the next film roll, pre-assembling format parts, printing labels and preparing the cleaning kit. Others need the line stopped, such as removing the old parts and fitting the new. Moving tasks from the second group to the first shortens the stop without changing what gets done. Quick-release format parts and recorded standard settings, so no one hunts for the right seal temperature, shorten what’s left.
Larger batches have costs too. They build inventory, tie up warehouse space, use up shelf life on finished goods, and lengthen the lead time for customers who order small quantities. If a product sells slowly, a long run produces stock that sits. So don’t default to big batches. Work out what a changeover costs, work out what extra stock costs, and compare them.
How to record changeovers
You can’t manage what you only estimate. A short log, filled in by the operator at each change, is enough to start.
Scroll horizontally to see all columns.
| Date | From product | To product | Stop time | First good pack | Back at target speed | Packs or film wasted | Reason for delays |
|---|---|---|---|---|---|---|---|
| (date) | (product A) | (product B) | (hh:mm) | (hh:mm) | (hh:mm) | (count or meters) | (short note) |
Three readings matter. The gap from stop to first good pack shows the setup and trial work. The gap from first good pack to target speed shows the ramp, the part most often left out. The waste count gives the setup material. Add a few words on reasons, such as “waited for film” or “seal temperature adjusted twice”, and patterns appear within a few weeks. Use the average in your model, but keep the range too, because a changeover that sometimes takes 40 minutes costs more than the average suggests.
Where it changes an automation decision
A faster rated machine isn’t automatically the better buy on a high-mix schedule. Compare two machines on the same shift as above, with the 30 minutes of other downtime kept and setup waste left out for clarity.
Machine X has an effective running rate of 42 good packs per minute and a 45-minute changeover. Machine Y runs at 35 and changes over in 15 minutes.
Scroll horizontally to see all columns.
| Changeovers per shift | Machine X good packs | Machine Y good packs |
|---|---|---|
| 2 | (480 - 90 - 30) x 42 = 15,120 | (480 - 30 - 30) x 35 = 14,700 |
| 4 | (480 - 180 - 30) x 42 = 11,340 | (480 - 60 - 30) x 35 = 13,650 |
At two changeovers X leads by 420 packs. At four, Y leads by 2,310. The crossover is where (450 - 45N) x 42 = (450 - 15N) x 35, which gives 18,900 - 1,890N = 15,750 - 525N, so N = 3,150 / 1,365 = about 2.3 changeovers per shift. Above that, the slower machine delivers more good packs. It’s the same bottleneck logic as before, applied to changeover loss. For the wider choice between manual, semi-automatic and automatic setups, see Manual, Semi-Automatic or Fully Automatic Packaging? A Cost Model.
Equipment that runs few hours changes this again, because idle time dilutes any speed advantage. How Equipment Utilization Changes Automation Payback covers that effect.
When the conclusion changes
The model matters most for mixed schedules. If the line makes one product for weeks, changeovers are rare and this article barely applies. If demand is for many small orders, the question becomes how to shorten changeovers, not how to avoid them.
It also changes when the line isn’t the constraint. If an upstream stage or the case packer limits output, lost minutes on a faster stage may cost nothing, so check which stage is the bottleneck before spending on quick-change parts. Other articles on this theme are collected under Production Economics. Unplanned stops aren’t modeled here; Measuring the Cost of Unplanned Production Downtime shows how to value them.
Keep reading
- Cost per Good Pack: A More Useful Measure Than Nameplate Speed: defines the cost measure and the no-double-counting rule used above.
- Why Faster Machines Do Not Always Increase Line Output: shows how the bottleneck stage sets the effective rate used in the model.
- Manual, Semi-Automatic or Fully Automatic Packaging? A Cost Model: compares setups at different volumes and product mixes.
Assumptions and limits
- The shift cost, waste and changeover length are examples. Real ones depend on the product pair and the crew.
- Every changeover is treated as 25 minutes and 60 packs. Real changeovers vary with the product pair, and a log will show the spread.
- Inventory, shelf life, storage space and customer lead times are not priced, though they matter when choosing batch size.
- Shift labor and overhead are held fixed. Overtime, extra cleaning labor and wear from more frequent changes could raise them.
- The machine comparison ignores setup waste, purchase price, financing, taxes and ramp-up, and assumes the machine is the bottleneck of the line.
- Use this to compare options, not as financial, legal, safety or engineering advice.