 WonksAnonymous
How to Calculate OEE for Multiple Machines: Bottleneck Pacemaker vs Simple Averages
Calculate OEE for multiple machines using constraint-based bottleneck line OEE for sequential lines and planned-production-time or volume weighting for parallel machines.
Deciding how to calculate OEE for multiple machines depends on whether the equipment operates as an autonomous parallel fleet or as a connected sequential production line. Taking a simple arithmetic average of machine OEE scores across a sequential line hides the bottleneck station that governs actual sellable output.
In Fabrico’s multi-machine OEE guide, simple average OEE—the sum of machine OEEs divided by the number of machines, such as five machines at 82%, 78%, 85%, 71%, and 88% giving 80.8%—is valid only for autonomous independent machines (such as 12 CNC machining centers in a job shop) and is misleading for sequential production lines where the output of one station feeds the next. In Harmony AI’s bottleneck analysis, averaging a constraint machine at 65% OEE with four non-constraint machines at 90% OEE produces a comfortable 85% plant-average OEE that hides the only number that limits sales, while non-bottleneck machines show low Availability and Performance because they are starved or blocked by the constraint rather than failing. Because sequential line availability is limited by the bottleneck station, Guidewheel notes that line-level OEE is typically 10-25 percentage points lower than the best individual machine on that line.
Use this guide alongside the production economics collection to select the right multi-machine aggregation formula, set ideal cycle times per product, classify starvation and blocking in Availability, and structure an Excel workbook without simple-average distortion.
Scroll horizontally to see all columns.
| Multi-Machine Configuration | Correct Aggregation Method | Mathematical Formula & Boundary | Worked Benchmark Example |
|---|---|---|---|
| Autonomous independent machines in a job shop | Simple average OEE across independent units | Sum of machine OEEs divided by the number of machines; misleading for production lines where stations operate in sequence and the output of one station feeds the next | In Fabrico’s example, five machines reporting OEEs of 82%, 78%, 85%, 71%, and 88% yield a simple average OEE of 80.8% (valid for 12 CNC machining centers running independent jobs) |
| Sequential production line (Constraint / Pacemaker method) | Constraint-based line OEE at the bottleneck station | Measure availability, performance, and quality at the constraint machine that limits line sales | In Harmony AI’s constraint example (450 minutes planned production time, 63 minutes own downtime and changeovers, 22 minutes starved, 387 minutes run time, 60-unit-per-minute ideal rate, 19,800 total units, 19,206 good), Availability is 86.0%, Performance is 85.3%, Quality is 97.0%, and OEE is 71.1% |
| Sequential VFFS packaging line shift | Compound three-factor line OEE | Final Line OEE = Availability × Performance Rate × Quality Rate across end-of-line shift counts | In WonksAnonymous’s VFFS packaging line example (21,870 packs run vs 24,300 packs theoretical = 90.0% Performance Rate, 875 rejected packs leaving 20,995 Good Output Packs = 96.0% Quality Rate), Final Line OEE is 0.90 × 0.90 × 0.96 = 77.76%, leaving more than 22% of line capacity unharvested |
| Multiple shifts or parallel machines with unequal scheduled duration | Planned-Production-Time-Weighted OEE | Combined OEE = Σ (OEE × planned production time) ÷ total planned production time | In LeanSuite’s three-shift rollup (scores of 75, 65, and 80 percent over 480, 480, and 240 planned minutes), weighted OEE is (360 plus 312 plus 192) ÷ 1,200 = 864 ÷ 1,200 = 72 percent versus a 73.3 percent simple average |
| Parallel lines with different production volumes | Production-Volume-Weighted Facility OEE | Weight each line’s OEE by its shift production volume rather than taking an unweighted average | In Fabrico’s two-line facility example, Line A producing 1,000 units per shift at 78% OEE and Line B producing 500 units per shift at 85% OEE give a weighted average facility OEE of 80.3% |
Why simple arithmetic averaging fails on sequential production lines
On a connected production or packaging line, station outputs are physically coupled, so overall line throughput cannot exceed the effective output rate of the slowest bottleneck stage. Averaging upstream and downstream machine percentages treats dependent stations as if their capacities were interchangeable.
In our machine speed and line throughput analysis, a four-stage packaging line model shows that the Case packer (rated speed 50, Availability 0.80, Performance 0.90, Quality 0.99, effective rate 35.64 good packs per minute) has the lowest effective rate below the Bagger (rated 60, Availability 0.90, Performance 0.95, Quality 0.98, effective rate 50.27 rounded), making the case packer the bottleneck and setting line output at 35.64 good packs per minute or 17,107 good packs per 480-minute shift. In that four-stage upgrade comparison, Option A—replacing the bagger with a faster model rated at 80 packs per minute and raising its effective rate to 67.03 good packs per minute—leaves shift output unchanged at 17,107 packs (a change of zero), whereas Option B—keeping the bagger and raising the case packer’s availability from 0.80 to 0.90—raises line output to 40.10 good packs per minute rounded or 19,246 packs per shift (+2,139 or +12.5%).
A five-stage liquid packaging line illustrates the same physical ceiling. In Zonesun Auto Pack’s 5-stage bottling line example (Bottle Unscrambling 80 BPM, Filling 60 BPM, Capping 70 BPM, Labeling 75 BPM, and Case Packing 55 BPM), the case-packing system is the bottleneck restricting Maximum Line Capacity to 55 BPM, which equals 2,805 bottles per hour at 85% efficiency (55 × 60 × 0.85 = 2,805), while an accumulation table holding 300 bottles on a 60 BPM line provides 5 minutes of buffer time (300 ÷ 60 = 5 minutes).
Even when primary fillers and baggers appear unconstrained, shared back-end equipment can govern multi-line plant throughput. In Soontact Intelligent Equipment’s packaging line equipment selection checklist, across a 2026 pharmaceutical line benchmark plant-reported OEE ran a median of roughly 14 points above sensor-measured OEE, and in a food plant running around the clock across fifteen lines that shared four stretch wrappers and four palletizers, the true bottleneck sat at the shared back-end equipment rather than the primary machines.
Two valid methods for sequential multi-machine line OEE
Standards for manufacturing operations management anchor equipment indicators to defined work units; industry methods measure a connected line at the bottleneck pacemaker or at the end-of-line discharge boundary.
Under International Organization for Standardization (ISO) standard ISO 22400-1:2014, an industry-neutral framework specifies how to define, compose, exchange, and use key performance indicators (KPIs) for manufacturing operations management (MOM), as defined in IEC 62264-1 for batch, continuous, and discrete industries. ISO 22400-2:2014 (Automation systems and integration — Key performance indicators (KPIs) for manufacturing operations management — Part 2: Definitions and descriptions) is Edition 1, published in 2014-01. With reference to equipment, the KPIs in ISO 22400-2:2014 relate to work units, as specified in IEC 62264.
Vorne Industries defines the simplest way to calculate OEE as the ratio of Fully Productive Time to Planned Production Time—OEE = (Good Count × Ideal Cycle Time) / Planned Production Time—while the preferred calculation multiplies the three OEE factors: OEE = Availability × Performance × Quality. Keeping the three factors visible prevents a rising headline score from concealing scrap: in Vorne’s sequential two-week comparison, total OEE rose from 85.1% in Week 1 (90.0% Availability, 95.0% Performance, 99.5% Quality) to 85.7% in Week 2 (95.0% Availability, 95.0% Performance, 95.0% Quality), showing that a higher headline OEE can mask a 4.5% drop in Quality alongside a 5.0% gain in Availability. For a single-machine breakdown of those factors, see Calculating OEE on Packaging Lines: Availability, Performance, and Quality.
Bottleneck / pacemaker constraint OEE
Constraint-based line OEE measures the line against the design capacity of the bottleneck station. In Fabrico’s multi-machine OEE guide, constraint-based line OEE is calculated as actual line output divided by theoretical maximum line output, where theoretical maximum is based on the design capacity of the bottleneck station running at 100% OEE (Line A producing 1,000 units per shift at 78% OEE and Line B producing 500 units per shift at 85% OEE illustrate the contrasting volume-weighted approach at 80.3% for parallel lines).
When computing OEE at the constraint station, separate the constraint’s own stops from upstream starvation in the diagnostic log while tracking total output against the constraint’s ideal rate. In Harmony AI’s constraint OEE example—with 450 minutes planned production time, 63 minutes of its own downtime and changeovers, and 22 minutes it sat starved by an upstream failure—Run time for Availability is 450 − 63 = 387 minutes, and at a 60-unit-per-minute ideal rate with 19,800 total units and 19,206 good units, Availability is 387 ÷ 450 = 86.0%, Performance is 19,800 ÷ (387 × 60) = 85.3%, Quality is 19,206 ÷ 19,800 = 97.0%, and constraint OEE is 71.1%.
End-of-line packaging system boundary OEE
For an integrated packaging line with intermediate accumulation buffers, taking every count and stoppage after the final inspection station measures true end-of-line system performance. In Soontact Intelligent Equipment’s packaging line OEE guide, for a line rather than a single machine, every count and every stoppage is taken at the line’s output after the last inspection station—the checkweigher or metal detector—so an upstream jam that the buffer absorbs and that never stops the output is not a line loss at all, whereas one that starves the output is a line loss. At that discharge boundary, Vorne Industries defines OEE Quality similarly to First Pass Yield, where Good Parts are parts that successfully pass through the manufacturing process the first time without needing any rework: Quality = Good Count / Total Count.
In WonksAnonymous’s VFFS packaging line shift example (21,870 packs run divided by 24,300 packs theoretical = 90.0% Performance Rate, and 875 packs rejected subtracted from 21,870 packs = 20,995 packs Good Output Packs or 96.0% Quality Rate), Final Line OEE is 0.90 × 0.90 × 0.96 = 77.76%, leaving more than 22% of line capacity unharvested. Similarly, in Wolf-Packing’s jar packaging line analysis, a line with a 250 PPM designed engineering speed drops to 210-220 PPM running speed due to micro-stops, starvation, and blockages (12-16% loss), 180-195 PPM OEE-based speed after planned and unplanned stops reduce availability, and 170-185 PPM good-output speed after quality rejects, while SMED methodology reduced changeover time from 90 to 9 minutes (88% reduction), unlocking 3.55 hours of new production time daily.
OEE availability calculation: schedule loss, starvation, and blocking
An accurate OEE availability calculation starts by separating unscheduled calendar hours (which belong to TEEP Utilization) from Stop Time inside Planned Production Time.
In Vorne Industries’ OEE calculation guide, OEE Availability is calculated as Availability = Run Time / Planned Production Time, where Run Time = Planned Production Time − Stop Time, and Stop Time is defined as all time where the manufacturing process was intended to be running but was not due to Unplanned Stops (such as Breakdowns) or Planned Stops (such as Changeovers). Under Vorne Industries’ Six Big Losses framework, Equipment Failure is an Availability Loss that includes breakdowns, lack of operators or materials, being starved by upstream equipment, or being blocked by downstream equipment, for example using a two-minute policy threshold so any downtime longer than two minutes has a reason associated with it and is considered Equipment Failure. In the same Six Big Losses framework, Setup and Adjustments is an Availability Loss, whereas Idling and Minor Stops (typically a minute or two, well under five minutes) and Reduced Speed are Performance Losses, and Process Defects and Reduced Yield are Quality Losses.
Compare these two worked single-shift Availability and OEE calculations before building a multi-machine log:
Scroll horizontally to see all columns.
| Worked Shift Case | Time & Availability Breakdown | Speed, Quality & Resultant OEE |
|---|---|---|
| Vorne Industries widget shift — Availability | 480 minutes Shift Length minus 60 minutes Breaks = 420 minutes Planned Production Time | Subtracting 47 minutes Stop Time yields 373 minutes Run Time and 88.81% Availability (373 minutes / 420 minutes = 0.8881) |
| Vorne Industries widget shift — Performance, Quality & OEE | 373 minutes Run Time at a 1.0 seconds Ideal Cycle Time (60 parts per minute Ideal Run Rate) | 19,271 widgets Total Count minus 423 widgets Reject Count = 18,848 widgets Good Count, giving 86.11% Performance ((1.0 seconds × 19,271 widgets) / (373 minutes × 60 seconds)), 97.80% Quality (18,848 widgets / 19,271 widgets), and 74.79% OEE (0.8881 × 0.8611 × 0.9780 = 0.7479) |
| LeanSuite filling-line shift — Full OEE calculation | 480 minutes of planned production time, 30-minute unplanned stop plus 15-minute changeover = 45 minutes stop time, 435 minutes run time, and 90.6 percent Availability | At 0.5 minutes per unit ideal cycle time (870 units ideal output), 740 units filled with 22 rejected leaves 718 good units, giving 85.1 percent Performance, 97.0 percent Quality, and 74.8 percent OEE |
Separating OEE Availability from TEEP Utilization and macro capacity
Unscheduled shifts, holidays, and lack of orders reduce equipment Utilization in TEEP, not OEE Availability. In Vorne Industries’ TEEP guide, Total Effective Equipment Performance is calculated as TEEP = OEE × Utilization, where Utilization = Planned Production Time / All Time; for a plant at 65.00% OEE running two 8-hour shifts per day for 5 days per week (80 hours Planned Production Time out of 168 hours All Time across 24 hours × 7 days), Utilization is 47.62% (80 hours / 168 hours) and TEEP is 30.95% (0.6500 × 0.4762). Vorne notes that even a world-class manufacturing plant operating around the clock typically achieves only 80% to 90% Utilization of total capacity.
At the macroeconomic level, the Federal Reserve Board’s G.17 capacity indexes are constructed for 89 detailed industries (71 in manufacturing, 16 in mining, and 2 in utilities) and capture sustainable maximum output—the greatest level of output a plant can maintain within the framework of a realistic work schedule, after factoring in normal downtime and assuming sufficient availability of inputs. U.S. manufacturing capacity utilization was 75.7% in May 2026 per the Federal Reserve’s G.17 release, as cited in Harmony AI’s constraint benchmarking guide. See Manufacturing Capacity Utilization: Why the National Rate Is Not a Plant Target for how G.17 macro utilization differs from shop-floor OEE.
Empirical downtime drivers and maintenance economics
Plant downtime logs show why separating schedule losses from mechanical, electrical, and supply stops is essential:
- Downtime event durations by category: Across Guidewheel’s FactoryOps dataset of over 3,000 machines and 14,000+ downtime events, the average duration per downtime event is 318 minutes for No Business/Orders, 72 min for Mechanical breakdowns, 81 min for Other operational issues, 85 min for Maintenance & cleaning, 107 min for Electrical & controls, 197 min for Staffing issues, and 119 min for Material & supply issues.
- Packaging industry KPI tracking: In PMMI’s June 2026 Overall Equipment Effectiveness Quickie Survey (based on a May 2025–June 2026 quickie survey of 35 industry respondents), 45.7% of respondents currently offer customers a solution tracking Overall Equipment Effectiveness, 93.8% report downtime as the most commonly tracked KPI among current OEE offerings, and 100.0% of $250 Million plus respondents selected predictive maintenance metrics as an underserved capability.
- U.S. manufacturing maintenance expenditures and preventable losses: In NIST’s Economics of Manufacturing Machinery Maintenance report, 2016 machinery maintenance expenditures for NAICS 321-339 (excluding 324 and 325) were estimated to be $57.3 billion, with additional expenditures due to faults and failures estimated at $16.3 billion and costs for inventory to buffer against maintenance issues at $0.9 billion, totaling $74.5 billion. In the same NIST report, 2016 losses due to preventable maintenance issues amounted to $119.1 billion: $18.1 billion due to downtime, $0.8 billion due to defects, and $100.2 billion due to lost sales from delays and defects.
- Reactive versus preventive and predictive maintenance: NIST’s manufacturing machinery maintenance study found that the top 25 % of manufacturing establishments relying on reactive maintenance were associated with 3.3 times more downtime, 16.0 times more defects, and 4.9 times more inventory increases due to maintenance issues than the bottom 25 %, with 45.7 % of machinery maintenance being reactive on average. Conversely, establishments that invested more heavily into preventive or predictive maintenance had on average 44 % less downtime, a 54 % lower defect rate, 35 % fewer lost sales due to defects from maintenance, and 29 % less lost sales due to delays from maintenance issues. To value an hour of line stoppage in dollars, see Measuring the Cost of Unplanned Production Downtime.
How to calculate ideal cycle time in OEE across single-SKU, multi-nozzle, and multi-format shifts
Ideal Cycle Time is the fastest cycle time a process can achieve under optimal circumstances, and setting it incorrectly distorts the entire Performance factor.
In Vorne Industries’ OEE calculation guide, OEE Performance is calculated as Performance = (Ideal Cycle Time × Total Count) / Run Time or Performance = (Total Count / Run Time) / Ideal Run Rate, where Ideal Cycle Time is the fastest cycle time that the process can achieve in optimal circumstances; Performance should never be greater than 100%, and if it is, that usually indicates that Ideal Cycle Time is set incorrectly (too high). In Fabrico’s Ideal Cycle Time guide, Ideal Cycle Time must be set per product (not per machine) from the manufacturer’s nameplate rate or demonstrated best sustained rate, whereas the classic error is using the average achieved cycle time as the ideal—which makes the performance factor always look close to 100% and causes speed losses, minor stops, and slow running to vanish from the data.
Multi-nozzle and multi-lane filling cycle time calculation
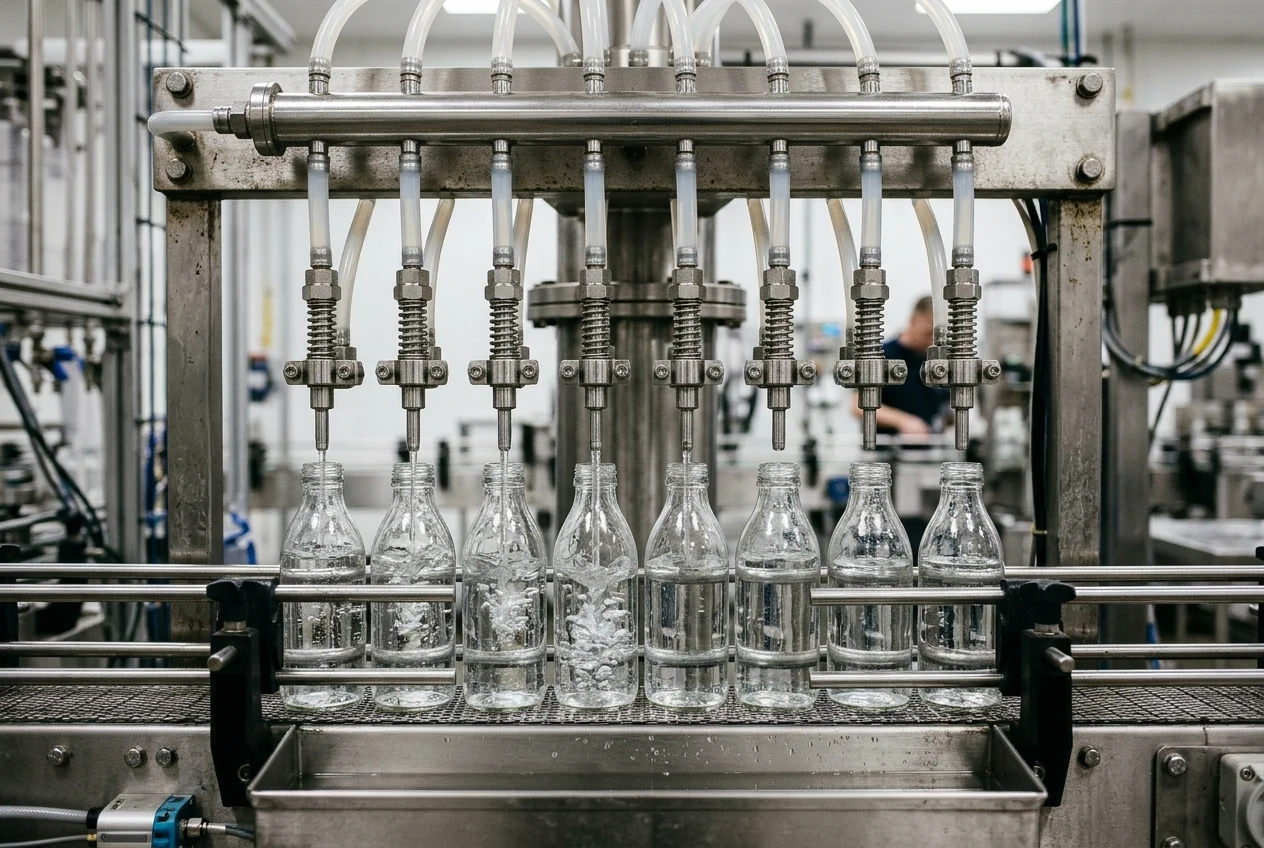
On multi-lane or intermittent multi-head machinery, convert the multi-unit machine cycle into a per-container rate before computing shift output. In Zonesun Auto Pack’s bottling line capacity guide, for an eight-nozzle filling machine that completes one cycle every 12 seconds, Filling Capacity is 8 × 60 ÷ 12 = 40 BPM, which equals a theoretical hourly capacity of 40 × 60 = 2,400 bottles per hour or 2,040 bottles per hour at 85% efficiency (2,400 × 0.85), and across 420 minutes of available time at 85% efficiency and a 1% reject rate (0.99), actual output is 40 × 420 × 0.85 × 0.99 = 14,137 acceptable bottles per shift.
Multi-SKU / multi-format shifts: summing ideal time instead of averaging speed
When a line runs two or more SKU formats with different ideal speeds during the same shift, applying a single cycle time or averaging the speeds distorts Performance. In Soontact Intelligent Equipment’s packaging line OEE guide, when two or more formats with different ideal speeds share a shift, Performance must be calculated from the ideal time each product’s packs should have taken, summed and divided by run time, rather than from a count-weighted average speed, because an average of speeds is not the same as a sum of times and the slower product takes a larger share of the minutes than of the packs.
Parallel machines & multi-shift rollups: how to calculate OEE for multiple machines in Excel
When aggregating autonomous parallel machines or multiple shifts in Excel, replace =AVERAGE() with a weighted formula (SUMPRODUCT) weighted by Planned Production Time or shift production volume.
- Planned-Production-Time-Weighted OEE (
Combined OEE = Σ (OEE × planned production time) ÷ total planned production time): In LeanSuite’s step-by-step OEE calculation guide, when three shifts (or parallel machine runs) score 75, 65, and 80 percent with planned production times of 480, 480, and 240 minutes (1,200total planned minutes), the simple average is 73.3 percent, whereas the time-weighted average is(360 plus 312 plus 192) ÷ 1,200 = 864 ÷ 1,200 = 72 percent. - Production-Volume-Weighted Facility OEE: In Fabrico’s multi-machine OEE guide, a facility with two parallel lines where Line A produces 1,000 units per shift at 78% OEE and Line B produces 500 units per shift at 85% OEE has a volume-weighted average facility OEE of 80.3%, whereas a sequential line requires constraint-based line OEE based on the bottleneck station running at 100% OEE.
- Auditing manual Excel OEE logs against sensor baselines: In Guidewheel’s OEE guide, operators using manual spreadsheets rarely log 30-second jams or sensor trips even though these typically account for 10-30% of total time loss across a shift, manual reporting typically captures only 50-75% of true OEE losses, and changeover variability across shifts averages 57%. In Fabrico’s multi-machine OEE guide, when unlogged micro-stops, unrecorded speed losses, and misattributed quality losses accumulate across five, ten, or twenty stations and are combined into a line or facility aggregate, the manual facility OEE figure may be 10 to 20 points above the actual machine-connected figure.
- Benchmarking multi-machine OEE scores realistically: In Vorne Industries’ World-Class OEE guide, if all three OEE factors (Availability, Performance, Quality) are 90%, the resultant OEE is only 73%; Seiichi Nakajima included the 85% World-Class OEE numbers in his 1984 book Introduction to TPM (translated to English and published in 1988 by Productivity Press), whereas most manufacturing companies have OEE scores closer to 60%, with more scoring lower than 45% than in excess of 85%.
Connecting multi-machine OEE to unit cost and the financial bridge
Raising OEE on a non-bottleneck station usually adds no sellable throughput unless that station was starving the constraint.
In OpenStax Principles of Managerial Accounting (Cost Behavior), total fixed costs remain unchanged within the relevant range while Average Fixed Cost (AFC = Total Fixed Costs / Total Units Produced) goes up and down with the number of units produced, and Average Variable Cost (AVC = Total Variable Costs / Total Units Produced) results in a constant per-unit cost. In OpenStax Principles of Managerial Accounting (Differential Analysis), only avoidable costs that differ between alternatives are relevant for short-run decision-making, whereas the book value of an existing asset (historical cost minus accumulated depreciation) is a sunk cost and irrelevant to the decision at hand. When an OEE gain eliminates weekend or after-hours catch-up shifts, federal overtime regulation 29 CFR § 778.107 (Fair Labor Standards Act section 7(a), 46 FR 7309, Jan. 23, 1981) requires that overtime be compensated at a rate not less than one and one-half times the regular rate at which the employee is actually employed.
In WonksAnonymous’s Overall Equipment Effectiveness Formula, Calculator, and the OEE Financial Bridge, raising a 4,000-hour, 3,000-pack/hour packaging line from 65.00% to 70.00% OEE always unlocks +600,000 good packs per year or frees 285.71 planned hours, with real annual cash impact ranging from $0 in fixed-cost savings ($3,000 in variable energy) under excess capacity, to $41,538 in eliminated overtime payroll, to +$117,000 in bottleneck EBITDA plus +$260,331 in present-value CapEx deferral (a 2-year delay on a $1.5M line at 10% WACC). To translate end-of-line good pack counts into unit operating cost without double-counting scrap, see Cost per Good Pack.
Frequently asked questions
Can you average OEE across multiple machines?
In Fabrico’s multi-machine OEE guide, a simple average OEE (such as five machines at 82%, 78%, 85%, 71%, and 88% giving 80.8%) is valid only for autonomous independent machines like 12 CNC machining centers in a job shop and is misleading for sequential production lines. In Harmony AI’s bottleneck analysis, averaging a constraint at 65% with four non-constraints at 90% produces a comfortable 85% plant-average OEE that hides the constraint limiting sales, because non-bottleneck machines show low Availability and Performance when they are starved or blocked by the constraint.
How do you calculate OEE for multiple machines or shifts in Excel?
For parallel machines or shifts with different scheduled durations, LeanSuite specifies weighting each score by Planned Production Time using Combined OEE = Σ (OEE × planned production time) ÷ total planned production time—for example, three shifts scoring 75, 65, and 80 percent over 480, 480, and 240 minutes yield (360 plus 312 plus 192) ÷ 1,200 = 864 ÷ 1,200 = 72 percent rather than a 73.3 percent simple average. For parallel lines with different output capacities, Fabrico weights each line by shift production volume (such as Line A producing 1,000 units per shift at 78% OEE and Line B producing 500 units per shift at 85% OEE, giving a weighted average facility OEE of 80.3%), whereas sequential lines use constraint-based line OEE based on the bottleneck station running at 100% OEE.
How do you calculate ideal cycle time in OEE for multi-nozzle or multi-SKU lines?
In Vorne Industries’ OEE guide, Ideal Cycle Time is the fastest cycle time the process can achieve in optimal circumstances (Performance = (Ideal Cycle Time × Total Count) / Run Time), and Performance exceeding 100% usually indicates Ideal Cycle Time is set too high. Fabrico states that Ideal Cycle Time must be set per product from the manufacturer’s nameplate rate or demonstrated best rate rather than average achieved speed (which makes Performance look close to 100% and hides speed losses). On a multi-nozzle filler, Zonesun Auto Pack calculates capacity for an eight-nozzle filling machine completing one cycle every 12 seconds as 8 × 60 ÷ 12 = 40 BPM (2,400 bottles per hour theoretical, 2,040 bottles per hour at 85% efficiency, and 40 × 420 × 0.85 × 0.99 = 14,137 acceptable bottles across 420 minutes at 1% rejects). When two or more formats with different ideal speeds share a shift, Soontact Intelligent Equipment specifies summing the ideal time each product’s packs should have taken and dividing by run time.
How do upstream starvation and downstream blocking affect OEE availability calculation?
In Vorne Industries’ OEE framework, Availability = Run Time / Planned Production Time, where Run Time = Planned Production Time − Stop Time across unplanned and planned stops. Under Vorne’s Six Big Losses framework, Equipment Failure is an Availability Loss that includes breakdowns, lack of operators or materials, being starved by upstream equipment, or being blocked by downstream equipment (for example using a two-minute policy threshold). In Harmony AI’s constraint OEE example (450 minutes planned production time, 63 minutes of own downtime and changeovers, and 22 minutes starved by an upstream failure, giving 387 minutes Run Time at a 60-unit-per-minute ideal rate with 19,800 total units and 19,206 good units), Availability is 86.0%, Performance is 85.3%, Quality is 97.0%, and constraint OEE is 71.1%.
Return to the production economics collection for related analyses on line throughput, downtime valuation, and unit cost.
Sources
- International Organization for Standardization — Automation Systems and Integration KPI Standards
- National Institute of Standards and Technology — Economics of Manufacturing Machinery Maintenance
- Vorne Industries — Calculating OEE (oee.com)
- Vorne Industries — Six Big Losses in Manufacturing (oee.com)
- Vorne Industries — Calculate TEEP (oee.com)
- Vorne Industries — World-Class OEE (oee.com)
- PMMI — Overall Equipment Effectiveness Quickie Survey
- Federal Reserve Board — Industrial Production and Capacity Utilization Explanatory Notes
- OpenStax — Principles of Managerial Accounting
- Electronic Code of Federal Regulations — General Standard for Overtime Pay
- Fabrico — How to Calculate OEE for Multiple Machines
- Fabrico — Ideal Cycle Time in OEE Manufacturing
- Harmony AI — OEE for Bottleneck Machines
- LeanSuite — OEE Calculation: Step-by-Step Guide
- Guidewheel — The Complete Guide to OEE
- Soontact Intelligent Equipment — How To Calculate OEE For Packaging Line
- Soontact Intelligent Equipment — Checklist For Selecting Packaging Line Equipment
- Zonesun Auto Pack — How to Calculate Bottling Line Capacity
- Wolf-Packing — Jar Line Speeds: Filling, Sealing, And Labeling Throughput
- WonksAnonymous — Calculating OEE on Packaging Lines
- WonksAnonymous — Why Faster Machines Do Not Always Increase Line Output
- WonksAnonymous — Overall Equipment Effectiveness Formula, Calculator, and the OEE Financial Bridge